


Contents
The old distinction between a handmade knife and a factory-made knife sounds simple: one is made by a craftsman, the other by machines. In the modern knife industry, that explanation is no longer very useful.
Custom makers use CNC machines, CAD, precision grinders, fixtures, professional heat-treatment services, and other modern equipment. Production manufacturers may rely on skilled workers for grinding, fitting, assembly, sharpening, and final inspection. A machine does not make a knife “less handmade,” just as hand assembly does not automatically make a production knife custom.
The better comparison is between two different manufacturing models.
Production is designed around repeatability, scalability, predictable cost, and the ability to make many examples of essentially the same knife. An individual maker or small workshop has greater freedom to spend time and money on decisions that only need to make sense for one knife or a small number of knives.
Both systems can produce excellent knives. Both can produce disappointing ones.
After more than a decade working with handmade knives, makers, engravers, collectors, and high-end knife projects, I have found that the label matters less than understanding what the manufacturing model allows — and what the buyer is actually paying for.
This distinction also explains why the handmade custom knives market is so broad. It includes practical working knives, precision folders, individually commissioned pieces, engraved knives, and one-of-one collector objects that may have very different reasons for existing.
Knife-industry terminology is less standardized than many buyers expect. There is no universal rule defining exactly how much handwork a knife needs before it can be called handmade, nor is there a regulated boundary separating custom, mid-tech, semi-custom, and production knives.
That makes the terminology useful as a starting point, but dangerous as a quality rating.
A handmade knife normally involves substantial direct work by an individual maker or small workshop. Grinding, fitting, handle shaping, finishing, assembly, engraving, sharpening, or other operations may be performed individually.
That does not mean the maker has to avoid modern machinery.
A maker can use CNC machining to produce a titanium component, a surface grinder to establish reference surfaces, or CAD to refine a folder design and still retain direct control over the finished knife. Machines are tools. What matters more is the scale of production, who controls the design, how critical operations are performed, and how much individual fitting and finishing each knife receives.
The term custom knife has several meanings in actual market use.
In the strictest sense, it can describe a knife made specifically to a customer’s specification. Dimensions, blade shape, materials, finish, engraving, and other elements may be agreed before construction begins.
Collectors also use custom more broadly for individually made or very low-volume maker knives, including one-of-one pieces designed entirely by the maker and offered for sale after completion.
That means custom does not necessarily mean commissioned.
We cover the terminology itself more fully in our guide to what a custom knife is. For this comparison, the important point is that custom work generally gives an individual maker substantially more control over a particular knife than conventional production allows.
A production knife is built around a repeatable design and manufacturing system. Components have established specifications, manufacturing operations are standardized, and the goal is to produce essentially the same functional product again and again.
Production does not mean cheap.
Modern factory knives can use premium powder steels, titanium, carbon fiber, sophisticated locking mechanisms, precision machining, controlled heat treatment, and very good finishing.
The word production describes how the knife is reproduced. It does not define its maximum quality.

The clearest way to understand the difference is to look at the question each manufacturing model has to answer.
A production manufacturer has to ask:
Can we reproduce this design reliably, at the required quality and cost, across an entire production run?
An individual maker can ask:
What makes sense for this particular knife?
That difference affects almost everything.
A factory knife needs dimensions and tolerances that work repeatedly. Parts may need to remain interchangeable. Materials must be available in useful quantities. Operations that add significant labor need to be justified across hundreds or thousands of knives. Warranty exposure, assembly time, serviceability, and manufacturing yield all matter.
A maker working on one knife does not face exactly the same constraints. A handle can be adjusted for a particular customer. An unusual piece of natural material can be used even if there is no possibility of sourcing another identical piece. More time can be spent refining an individual transition, fitting a component, altering proportions, or completing a finish that would be too expensive to reproduce at volume.
This is the key distinction throughout the article:
Production optimizes a repeatable product. Maker-led work can optimize an individual piece.
That does not tell us which knife will be better. It tells us why the two categories make different compromises.
For the actual sequence of professional knife construction — from design through grinding, heat treatment, assembly, finishing, and QC — see our separate guide to how a custom knife is made.
Production manufacturing has genuine advantages, especially when the knife is primarily a tool.
The most obvious advantage is consistency across a model.
Once a manufacturer has stabilized the design, machining programs, material specifications, heat-treatment requirements, assembly process, and quality-control standards, those processes can be repeated across a large number of knives.
Manufacturing defects still happen. Production QC is not infallible. But the system itself is designed to reduce uncontrolled variation.
If you buy two examples of the same established factory-made knife, you normally expect their dimensions, construction, hardware, steel, lock design, and basic performance characteristics to be very similar.
For many users, that predictability has considerable value.
Production also distributes development and tooling costs across many units.
A company can invest in CAD development, fixtures, molds, CNC programming, heat-treatment protocols, testing, and tooling because those costs are distributed across a production run.
An individual maker may spend several hours solving a problem that applies to one knife. That labor has to be paid for by the buyer of that knife.
As a result, a good production knife often offers extremely strong functional value per dollar. If your main requirement is a reliable EDC or working blade and you have no need for individual materials, personalized dimensions, or collector provenance, a high-quality production knife may be the more rational purchase.
Production knives are usually easier to replace.
That sounds mundane until the knife is a working tool.
If you damage or lose an established production model, another example may still be available. Replacement clips, screws, hardware, scales, or even blades may be obtainable through the manufacturer or aftermarket.
A one-of-one handmade knife can be literally irreplaceable.
For a collector, that uniqueness may be part of the appeal. For someone who depends on a knife every day, it can be a disadvantage.
Larger manufacturers can also support standardized warranty departments, inventories of spare parts, documented repair procedures, and established service policies.
An individual maker may provide exceptional personal service, but the capacity of that service is tied directly to one person or a small workshop.
Neither approach is inherently better. They solve different ownership problems.

The central advantage of maker-led work is freedom from large-scale production requirements.
That freedom can be used well or badly. In the hands of a skilled maker, however, it allows decisions that would be difficult to justify in conventional factory production.
A production knife normally needs to work for a broad range of users.
An individual maker can narrow the brief.
A hunting knife can be developed around a specific field task. A folder can prioritize a particular blade-to-handle ratio or carry profile. Handle dimensions can be adapted for a specific hand. A collector piece can use proportions or decorative construction that would make little economic sense in mass production.
The important word is specific.
Custom work is not automatically better geometry. It simply gives the maker more freedom to optimize geometry for a narrower purpose.
Large-scale production depends on predictable supply.
An individual maker can build around a single exceptional piece of stabilized wood, fossil material, specialist Damascus, Timascus, engraved titanium, or another material that may never be available in exactly the same form again.
The functional advantage may be small or nonexistent. The collector advantage can be substantial.
This is one of the clearest areas where comparing custom and factory knives only by cutting performance becomes misleading. A buyer may deliberately be paying for rarity, visual composition, craftsmanship, or provenance rather than another percentage point of practical utility.
Low-volume work also makes individual fitting economically possible.
A maker can spend additional time correcting a transition, tuning the action of a folder, adjusting a lock interface, refining a grind, or fitting decorative components because the individual attention itself is part of the finished product.
A useful example from our work is LesBar Knives. Their knives divide two very different disciplines between specialists: Oleh Lesuchevsky works on the engineering side — blade geometry, lock interfaces, tolerances, construction, and action — while Stan Baranovsky handles hand engraving, inlays, and the artistic treatment of the finished piece.
That division illustrates something often lost in the phrase handmade knife. A high-end maker-built knife does not necessarily represent one person avoiding machinery. It can represent several specialist disciplines coordinated around one object, with each stage receiving attention that would be difficult to standardize economically across a conventional factory run.

One of the strongest arguments in favor of production knives is consistency.
The argument is valid, but it is often simplified too far.
Production manufacturing is explicitly built around repeatability. The company wants knife number 50 and knife number 5,000 to remain within defined manufacturing specifications.
An individual maker may never make 5,000 identical examples. Statistical consistency across a large population may therefore be irrelevant to the workshop’s actual output.
That does not mean a maker operates without process control.
Experienced makers develop repeatable methods for grinding, heat treatment, fitting, assembly, finishing, sharpening, and inspection even when the knives themselves are intentionally different.
So I would not frame the issue as factory = consistent, handmade = inconsistent. The more accurate distinction is this:
Production quality depends heavily on the manufacturing system. Individual knife quality depends more directly on the maker’s process discipline and judgment.
A weak factory QC system can release defective knives. An undisciplined custom maker can produce attractive knives with poor geometry or mechanics. A strong manufacturer and a strong individual maker can both produce excellent results.
This is why “handmade” should never be used to excuse poor fit, unstable lockup, badly controlled grinding, or careless assembly.
If you are trying to assess the workmanship of a specific knife rather than choose between product categories, our knife fit and finish guide covers that question separately.

The modern knife market is not divided neatly into two camps.
There is a large middle ground between a one-off custom knife and conventional factory production.
| Category | Typical design model | Manufacturing model | Individual involvement | Buyer customization |
|---|---|---|---|---|
| Production | Standardized model | Repeatable volume production | Production assembly and QC | Usually limited |
| Semi-custom | Existing platform | Mostly standardized | Varies | Selected materials, finishes, or options |
| Mid-tech | Maker-led or small-batch design | Mix of scalable machining and maker or workshop operations | Often substantial | Varies widely |
| Full custom | Maker-specific or one-off | Individual or very small-volume construction | Extensive | Potentially extensive |
These terms overlap. They are not governed by a universal industry standard, so the label should never replace a description of how the knife was actually made.
Mid-tech is probably the most ambiguous term in this group.
Traditionally, it described knives positioned between full custom work and mainstream production. A maker might design the knife and retain control over critical finishing and fitting while some blanks or components were produced externally or by scalable machining.
Today that boundary is harder to see.
A small custom workshop can own sophisticated CNC equipment. A production manufacturer can use extensive hand finishing. Some supposedly mid-tech knives resemble low-volume production, while others retain substantial maker involvement.
For that reason, I place less value on the label than on the underlying facts.
Those answers are more useful than arguing about whether a particular knife technically qualifies as mid-tech.
No.
The word handmade describes a method or production context. It is not a quality grade.
A poorly made custom knife can have weak geometry, poor ergonomics, inconsistent heat treatment, rough transitions, unstable mechanical interfaces, or careless finishing.
A strong factory knife can have excellent geometry, controlled heat treatment, accurate machining, dependable lockup, good action, and consistent fit and finish.
The reverse is also true. An experienced individual maker can spend time refining one knife in ways that would add too much cost to an ordinary production model.
The mistake is using the category as a shortcut for evaluating quality.
The same principle applies to materials. Premium powder steels, titanium, carbon fiber, or Damascus can appear in both maker-built and production knives. Their presence does not prove which knife is better.
If steel choice is the actual question, use our guide to choosing the best knife steel rather than trying to infer performance from the handmade or factory-made label.
And once you have chosen the category that suits your needs, the next question is whether the specific knife is well executed. That is a different task, covered in our custom knife buying guide.
The price difference between a production knife and a maker-built knife is often described simply as paying for “better quality.”
That explanation misses much of the market.
At a certain level, both categories can provide all the functional performance many users realistically need. Spending more after that point may buy additional refinement, individuality, specialist craftsmanship, rarity, or provenance rather than a proportional increase in cutting ability.
A custom maker spreads design work, setup, fitting, finishing, sourcing, correspondence, corrections, and workshop overhead across very few finished knives.
Production spreads many of those costs across hundreds or thousands of units.
This is why two knives made from similar steel and titanium can have very different prices without either price necessarily being irrational.
A maker can devote several additional hours to a detail that would add an unacceptable unit cost to mass production.
That detail might be a mechanical adjustment, hand-rubbed finish, unusual material transition, individually fitted guard, custom engraving layout, or a change made specifically for one buyer.
Whether that work matters to you is a separate question.
At the upper end of the market, the knife may also become a platform for another craft.
Hand engraving, relief carving, gold inlay, scrimshaw, stone setting, specialist Damascus, and other decorative disciplines can add substantial labor without necessarily making the blade cut better.
That does not make the added cost artificial. It means the buyer is purchasing more than cutting performance.
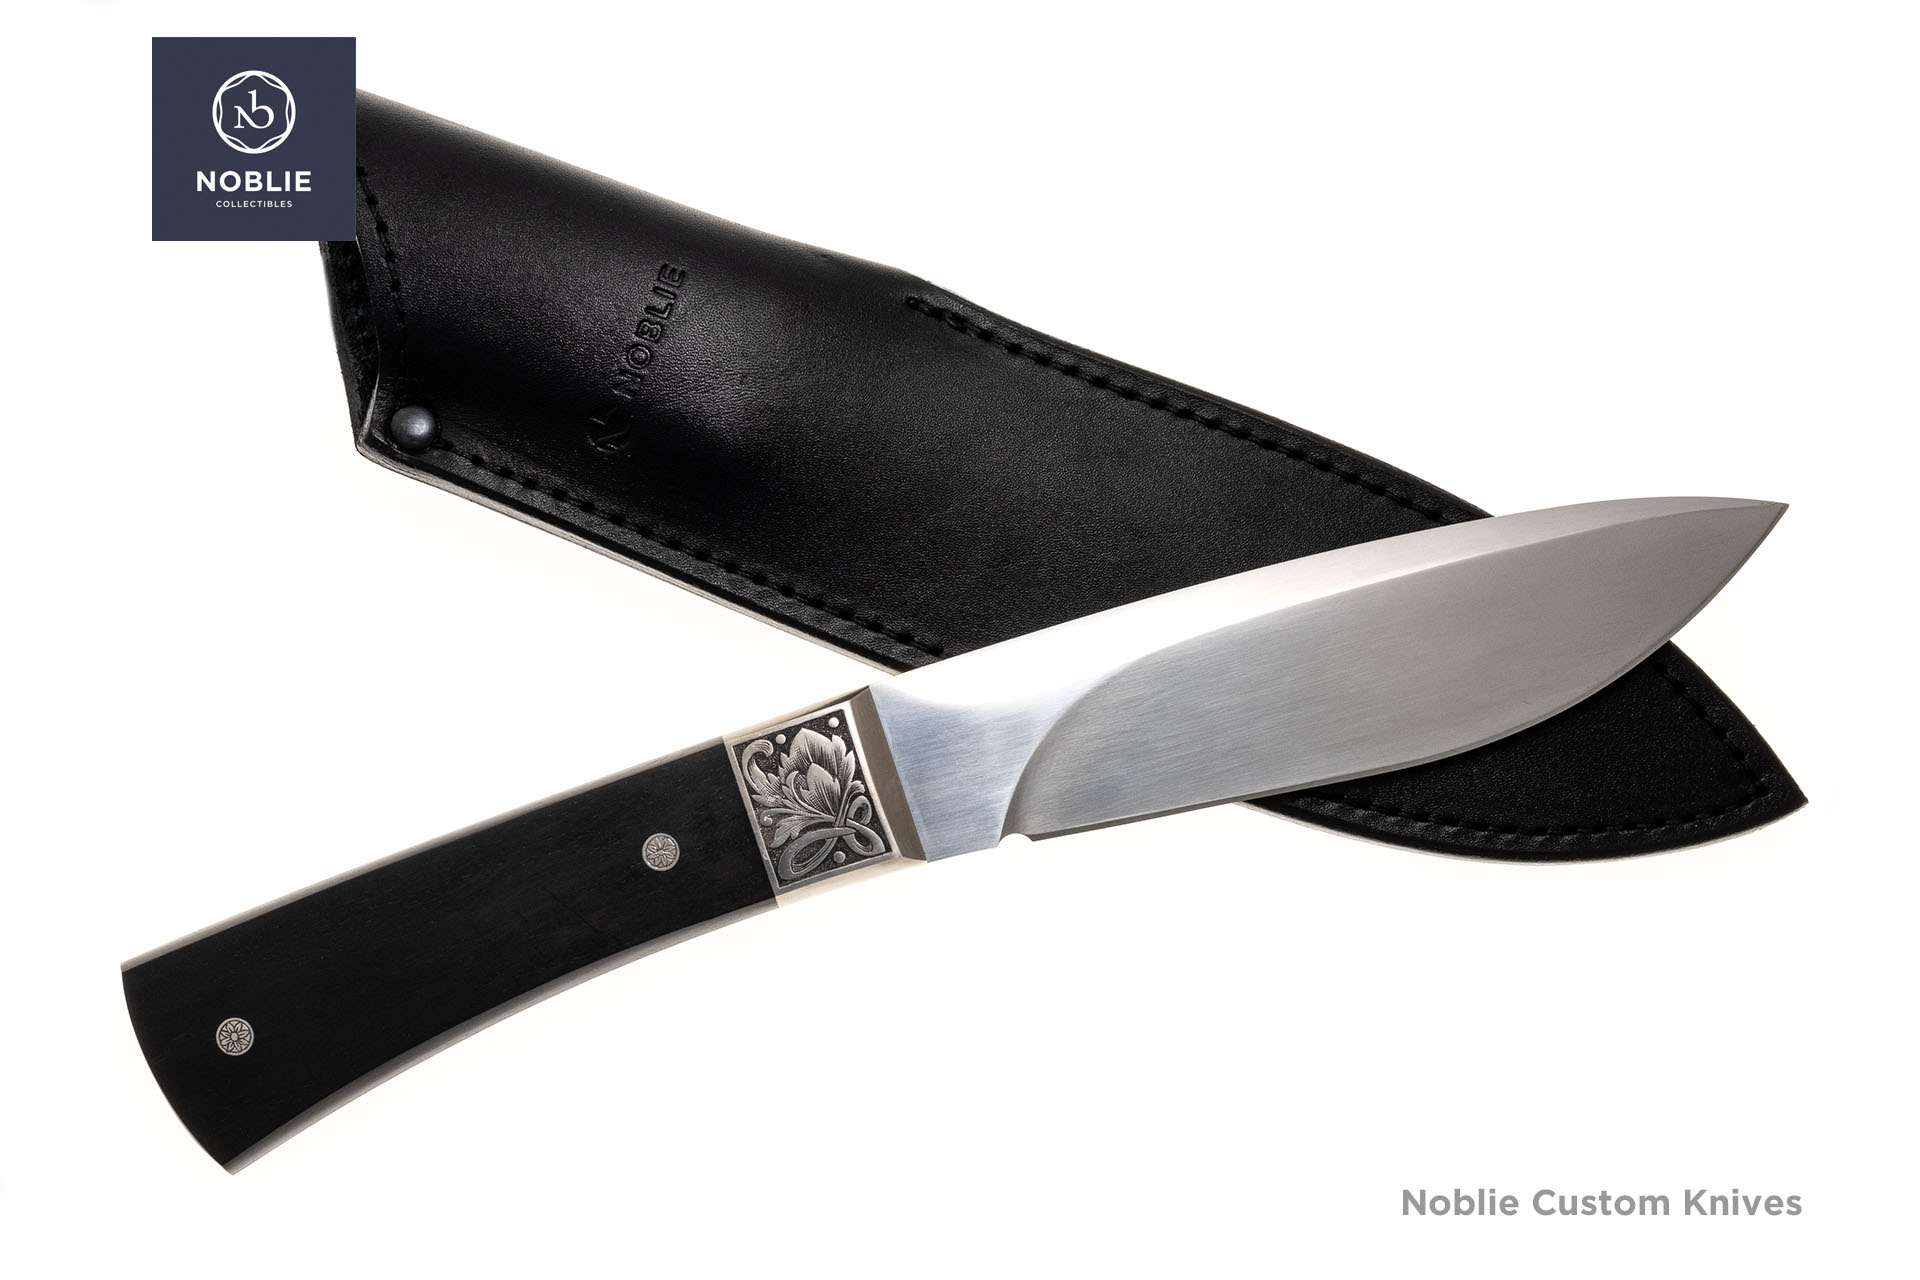
The distinction is especially visible in engraved knives and collector-grade art pieces, where mechanical knife construction and decorative craftsmanship become part of the same object.
A maker-built knife can also carry value because of authorship.
Who made it? Was it one of a small number produced? Is the configuration unusual? Was the engraving performed by a recognized specialist? Is the piece documented? Does it represent an important model or period in the maker’s work?
These are collector considerations rather than performance metrics.
This is why comparing a high-quality production EDC and a one-of-one art knife solely by edge retention misunderstands what the second buyer is purchasing.
For actual price ranges, rather than the reasons those prices differ, see how much a custom knife costs.

There is no universal winner. The more useful question is which manufacturing model matches your priorities.
| Your priority | More logical starting point |
|---|---|
| Maximum practical performance per dollar | Production |
| Easy replacement | Production |
| Standardized service and spare parts | Production |
| Established design with predictable specifications | Production |
| Specific dimensions or ergonomics | Custom / maker-built |
| One-of-one design | Custom |
| Rare or unusual materials | Custom / semi-custom |
| Personalized engraving or artistic work | Custom |
| Direct connection to a particular maker | Custom |
| Maker-led design with some repeatability | Mid-tech / semi-custom |
| Individual authorship and collector provenance | Maker-specific custom |
If I needed a working knife that I expected to use hard, replace easily, and service without difficulty, a good production model could be the rational choice.
If I wanted a particular maker’s design language, a knife built around unusual requirements, one-of-one materials, specialist engraving, or meaningful collector provenance, I would look toward custom or low-volume maker work.
Many buyers sit between those extremes. They want the confidence of an established design but also want more individual materials, finishing, or maker involvement than ordinary production offers. That is where semi-custom and mid-tech knives can make sense.
For buyers focused specifically on folders, our custom pocket knife collection shows how broadly maker approaches can differ within the same general product class.
The best rule is not “always buy handmade” or “production offers better value.” It is simpler:
Choose production when repeatability, price efficiency, availability, and standardized support are the priorities.
Choose maker-built work when individual design freedom, personalization, specialist craftsmanship, rarity, or provenance are part of what you actually want to own.
Not automatically. Handmade knives can allow greater individual fitting, design freedom, unusual materials, and direct maker involvement, but quality still depends on the skill and process control of the maker. High-quality factory knives can offer excellent geometry, machining, heat treatment, lockup, fit and finish, and reliability.
They can be, but only if you value what the extra cost buys. If your goal is primarily maximum cutting performance and reliability for the money, a good production knife may offer better value. A handmade knife becomes easier to justify when you value individual design, maker involvement, unusual materials, hand finishing, personalization, artistic work, rarity, or provenance. The premium should correspond to something you actually care about — not simply the word handmade.
A production knife is designed to be reproduced consistently as an established model. A custom knife generally involves substantially more individual maker control and may be one-of-one, made in very small numbers, or built to a customer’s specification. In collector usage, custom can also describe an individually maker-built knife that was not commissioned by its eventual owner.
Not as a category. Strength depends on blade steel, heat treatment, geometry, edge design, construction, and intended use. A production manufacturer or individual maker can optimize a knife toward toughness, cutting efficiency, corrosion resistance, or another performance priority.
Low production volume means that design, setup, individual fitting, finishing, sourcing, and workshop time are distributed across fewer knives. Custom pieces may also use unusual materials, one-off machining, hand engraving, specialist Damascus, carving, inlay, or other labor-intensive processes that would be difficult to reproduce economically in factory production.
Some do, especially work from makers with strong collector demand and well-documented provenance, but there is no guarantee. Resale depends on the maker, model, rarity, condition, configuration, documentation, and changes in collector demand. Handmade should not be treated as an automatic investment category.
A good production knife can be useful if you are still learning what blade length, handle geometry, carry weight, lock style, and overall format you prefer. It gives you a predictable reference point without requiring a large commitment. If you already understand your preferences and specifically value individual craftsmanship, maker identity, unusual materials, or customization, a handmade or custom knife may be the more satisfying choice.
About the author
Aleks Nemtcev is a knifemaker, collector, and founder of Noblie Custom Knives. He has more than ten years of practical experience working with handmade knives, collector pieces, Damascus steel, custom projects, engraving, and independent knifemakers.
His work includes evaluating knife construction, developing custom concepts, coordinating projects between knifemakers and decorative specialists, and selecting collector-grade knives for U.S. and international customers.


There are no comments for this article yet.